
Pharmaceutical drying equipment removes moisture and solvents to maintain the quality, stability, and effectiveness of medicines. Proper packaging then protects dried products from moisture, contamination, oxygen, and damage throughout storage and transportation.
Pharmaceutical drying equipment plays an important role in manufacturing medicines, powders, active pharmaceutical ingredients, and other drug products.
The main purpose of drying is to remove unwanted moisture and solvents while maintaining the quality, stability, and effectiveness of the product.
Different methods, including spray drying, vacuum drying, fluid-bed drying, and freeze drying, are selected according to the product and its requirements.
Growth
According to Towards Healthcare Researcha nd Consulting, the global pharmaceutical drying equipment market size is calculated at USD 5.84 billion in 2024, grew to USD 6.26 billion in 2025, and is projected to reach around USD 11.64 billion by 2034. The market is expanding at a CAGR of 7.14% between 2025 and 2034.
Role of Packaging in Pharmaceutical Drying Equipment
Packaging is an important step after the drying process because the dried product can quickly absorb moisture from the surrounding environment.
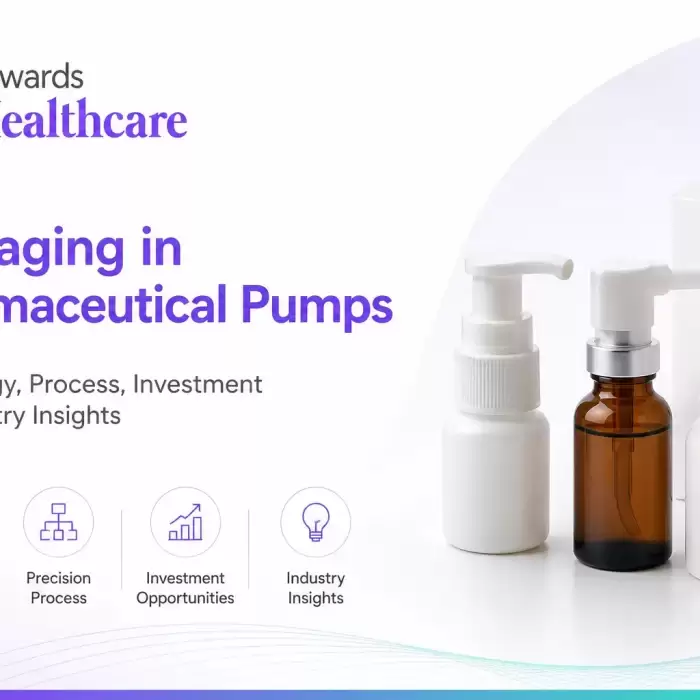
Proper packaging protects pharmaceutical products from moisture, oxygen, light, contamination, and physical damage during storage and transportation.
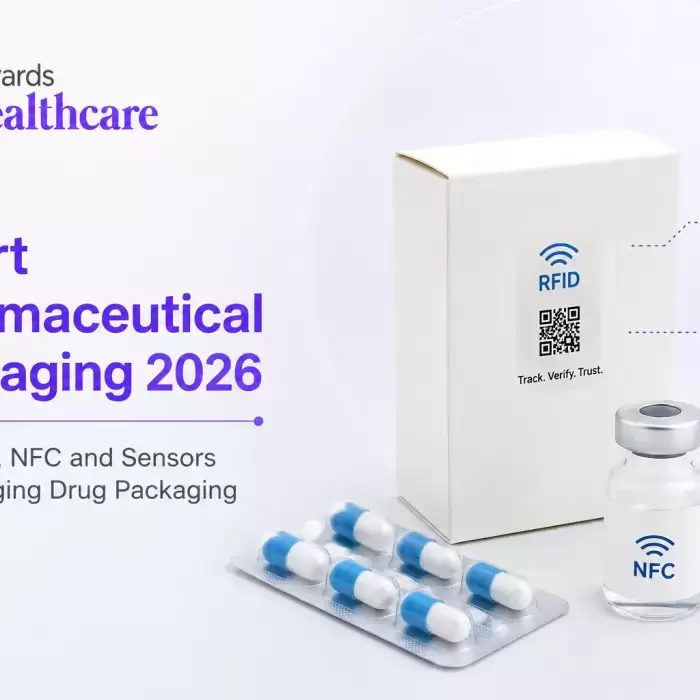
For moisture-sensitive products, manufacturers may use blister packs, bottles, sachets, pouches, vials, or other high-barrier packaging materials.
Good packaging also helps maintain product stability and extends shelf life while providing important information such as dosage, batch number, manufacturing date, and expiry date.
From Manufacturing to Packaging Process
The process starts with preparing the pharmaceutical material according to the required formulation and production specifications.
The material is then processed through suitable drying equipment to remove moisture or solvents under controlled temperature, pressure, and airflow conditions.
After drying, the product undergoes quality testing to check moisture content, purity, particle size, stability, and other important quality parameters.
Once the product meets the required standards, it moves to the packaging area under controlled manufacturing conditions.
The dried product is filled into the selected packaging, sealed properly, and checked for leakage, contamination, and packaging defects.
Finally, labels and batch details are added before the packaged medicines are sent for storage, distribution, and delivery.
Challenges in Drying and Packaging
One of the biggest challenges is moisture control. Poor drying or weak packaging can allow moisture to enter and affect the product's stability.
Manufacturers also need to control temperature, humidity, contamination, and equipment performance throughout the process.
Another challenge is selecting packaging materials that are compatible with the drug and provide sufficient protection throughout its shelf life.
Job Opportunities
This industry offers opportunities in pharmaceutical production, packaging operations, quality control, quality assurance, engineering, equipment maintenance, validation, and process development.
Professionals with knowledge of pharmaceutical manufacturing, GMP, drying technology, packaging systems, and quality standards can find opportunities in pharmaceutical companies and contract manufacturing organizations.
With increasing pharmaceutical production and demand for stable, high-quality medicines, expertise in both drying and packaging processes is becoming increasingly valuable.
References:
https://www.towardshealthcare.com/insights/pharmaceutical-market-sizing
https://www.towardshealthcare.com/

Comments (0)